
Solvent Recyclers
Showing all 7 results
-
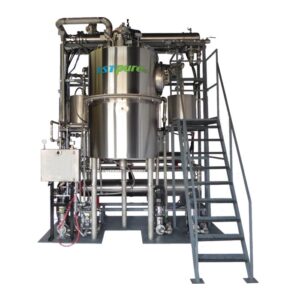
Kresco SRC Series Continuous-Flow Solvent Recyclers
Request a Quote -
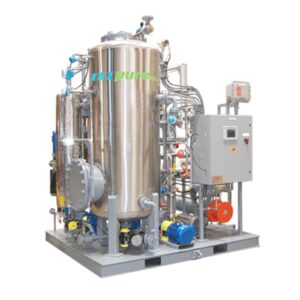
Kresco SRXC Distillation Columns
Request a Quote -

SR120 Solvent Recycler – 30-Gallon Class I Div I Solvent Reclaim System
Request a Quote -

SR180 Solvent Recycler – 48 Gallon
Request a Quote -
SR240 Solvent Recycler – 64 Gallon Class I Div I Solvent Reclaim System
Request a Quote -
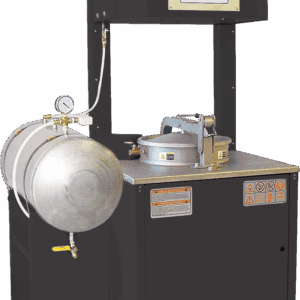
SR30V Solvent Recycler – 8 Gallon Class I Div I Solvent Reclaim System
Request a Quote -
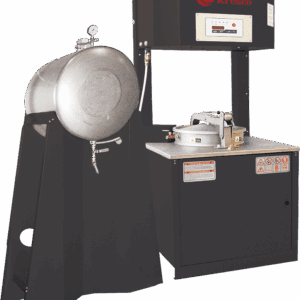
SR60V Solvent Recycler – 15 Gallon Class I Div I Solvent Reclaim System
Request a Quote
Industrial Solvent Recyclers
Reduce Solvent Costs, Hazardous Waste, and VOC Emissions
Industrial solvent recyclers are used to distill and reuse contaminated solvents generated from parts cleaning, spray gun washing, paint mixing, and surface preparation processes. By reclaiming usable solvent on site, facilities can significantly reduce hazardous waste disposal costs, lower fresh solvent purchases, and improve overall environmental compliance.
SolventRS offers a range of industrial solvent recycling systems designed for manufacturing, aerospace, automotive, defense, and industrial coating operations. Systems are available in multiple capacities and configurations to support common solvents such as acetone, MEK, mineral spirits, paint thinners, and other compatible cleaning fluids.
How Solvent Recycling Systems Work
Solvent recyclers use controlled distillation to separate reusable solvent from paint solids, coatings, oils, and other contaminants. The recovered solvent can then be reused in parts washers, spray gun cleaners, or other approved cleaning processes—reducing waste volume and operating costs.
Key advantages of on-site solvent recycling include:
Reduced hazardous waste disposal frequency
Lower solvent purchasing costs
Improved shop efficiency and uptime
Reduced VOC emissions and environmental impact
More predictable solvent management
Types of Solvent Recyclers Available
SolventRS offers both batch solvent recyclers and other industrial recycling configurations to match different production volumes and operational needs.
Batch Solvent Recyclers
Batch systems process solvent in defined cycles and are commonly used in small to mid-size paint shops and industrial facilities. These systems are cost-effective, reliable, and well-suited for operations with consistent but intermittent solvent waste generation.
👉 View available batch solvent recyclers to compare capacities and configurations.
Industries That Use Solvent Recyclers
Aerospace manufacturing and MRO facilities
Automotive and truck refinishing operations
Industrial paint and coating shops
Defense contractors
Manufacturing plants with parts cleaning processes
Why Buy a Solvent Recycler from SolventRS?
Industrial-grade systems designed for demanding environments
Support for common solvent chemistries used in coating operations
Equipment selected with safety, compliance, and longevity in mind
Application guidance to match recycler size and configuration to your process
Ongoing parts, service, and consumables support for ISTpure (now Kresco) and ECOpure solvent recyclers — including owners left without a source now that PPCTS, the original distributor, has closed. See our ISTpure & ECOpure parts and service page.
📩 Contact SolventRS for system selection assistance, specifications, and lead times.
Frequently Asked Questions
What is a solvent recycler used for?
A solvent recycler is used to distill and reuse contaminated solvents generated from cleaning, painting, and coating processes, reducing hazardous waste and solvent purchasing costs.
What solvents can typically be recycled?
Many industrial solvent recyclers support common solvents such as acetone, MEK, mineral spirits, paint thinners, and similar cleaning fluids. Compatibility depends on system design and application.
How do solvent recyclers reduce hazardous waste?
By reclaiming reusable solvent, recyclers reduce the volume of waste solvent that must be shipped off-site for disposal, lowering hazardous waste generation and handling costs.
Are solvent recyclers suitable for industrial and aerospace facilities?
Yes. Solvent recyclers are commonly used in industrial manufacturing, aerospace paint operations, automotive refinishing, and other regulated environments.
Is installation included with solvent recycling systems?
Installation, utilities, ventilation, and site preparation are typically the responsibility of the customer unless otherwise specified.
Is pricing listed on this page?
No. Pricing, lead times, and system configuration details are available upon request to ensure proper application and compliance.
Do you carry parts for ISTpure or ECOpure solvent recyclers?
Yes — Solvent Recycling Systems is a distributor and service partner for IST/Kresco (ISTpure) equipment, and we stock consumables and parts for ECOpure machines as well. Now that PPCTS, the original distributor for both brands, has closed, we’re one of the few remaining sources for bags, thermic oil, lid seals, condensers, and filtration for these units. See our ISTpure & ECOpure parts and service page for details.
Solvent Recycler Advantages
Durable: Built with robust, corrosion-free stainless-steel tanks.
Cost-effective: Most of our clients have achieved a return on investment (ROI) in as little as 4 to 12 months
Virtually Maintenance-Free: Require low maintenance and supervision, a simple 4-hour maintenance routine every 2,000 hours of operation.
Fully Automated Process: Operate on a fully automated process assisted by a PLC with predetermined parameter settings and built-in alarm signals.
Certified in North America: Certified to UL standard 2208 and CSA C22.2 No. 30 in Canada and the U.S. for class I, Div.1, Group D hazardous locations, and meets NFPA codes 30, 33, 70.
Guaranteed: Backed up by industry’s leading 2-year manufacturer warranty.
ISTpure-Brochure-Solvent-Recyclers (2)
Sizing a solvent recycler?
Start with our Solvent Recycler Buyer’s Guide: how solvent distillation works, sizing by gallons of dirty solvent per day, which solvents can be recycled, payback vs. hauling hazardous waste, and the recycler bags and heat-transfer oil you will need to keep it running.
